Trusted by Engineers and Researchers at Fortune 500 Companies for Precision Manufacturing
Trusted manufacturing experience with leading global companies.
Lockheed Martin
Sumitomo Electric Interconnect Products
Saint-Gobain Performance Plastics Pampus GmbH
3M
Frito-Lay
Parker Hannifin Corporation
Boston Scientific
General Dynamics – OTS Canada
ITW Food Equipment
Hemlock Semiconductor
Saft Batteries
KLA-Tencor
Land O'Lakes
Fastenal
Volvo Construction Equipment
Lockheed Martin
Sumitomo Electric Interconnect Products
Saint-Gobain Performance Plastics Pampus GmbH
3M
Frito-Lay
Parker Hannifin Corporation
Boston Scientific
General Dynamics – OTS Canada
ITW Food Equipment
Hemlock Semiconductor
Saft Batteries
KLA-Tencor
Land O'Lakes
Fastenal
Volvo Construction Equipment
Hand reamers are manual cutting tools that finish a drilled hole to an exact size and a smooth surface. A drill alone leaves a hole that is slightly oversize, rough and not perfectly round. A hand reamer removes a very small amount of material and produces a hole accurate to an H7 tolerance or better, ready for a dowel pin, bushing or shaft.
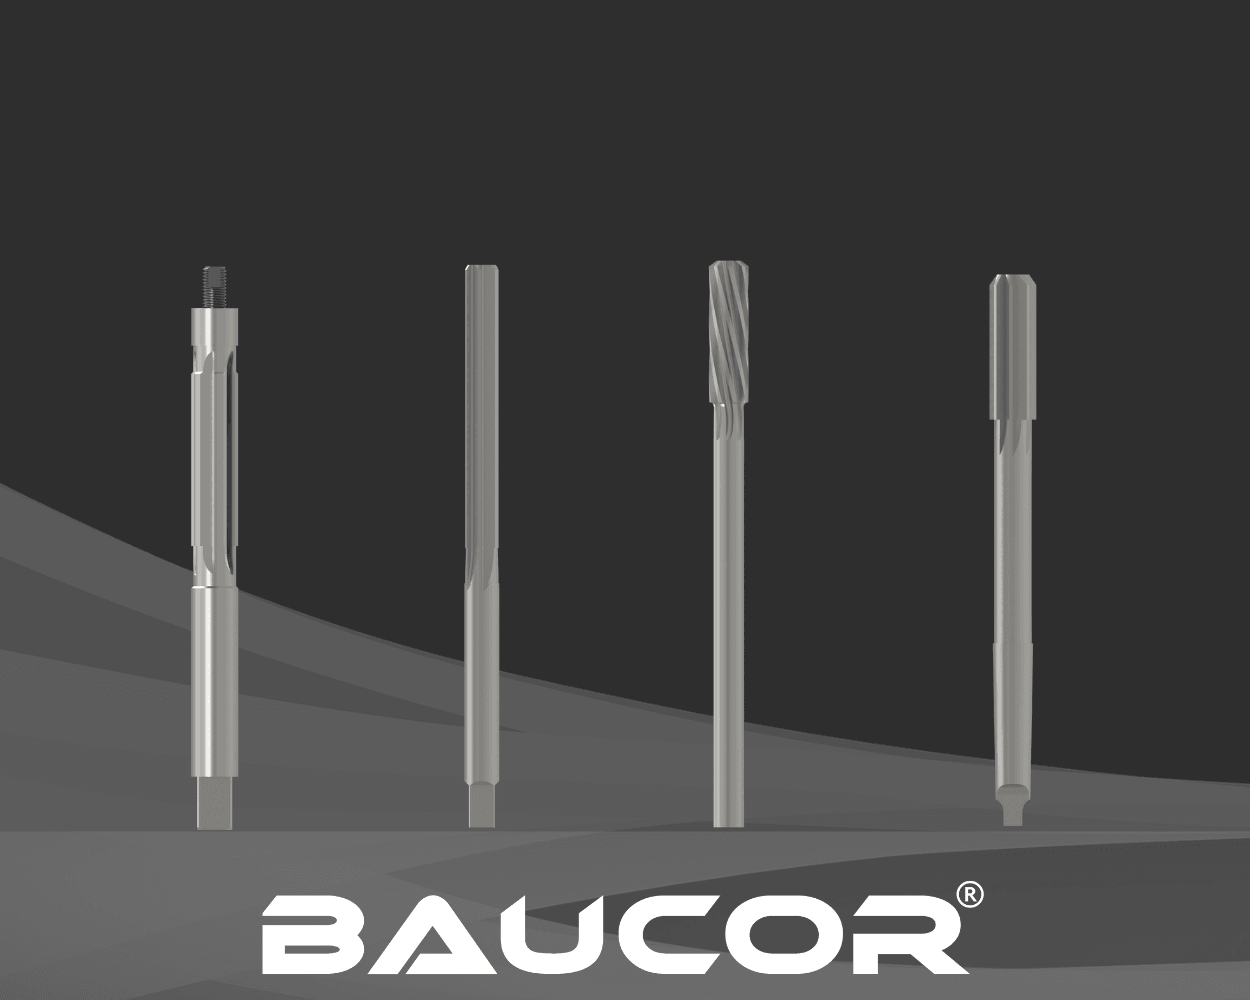
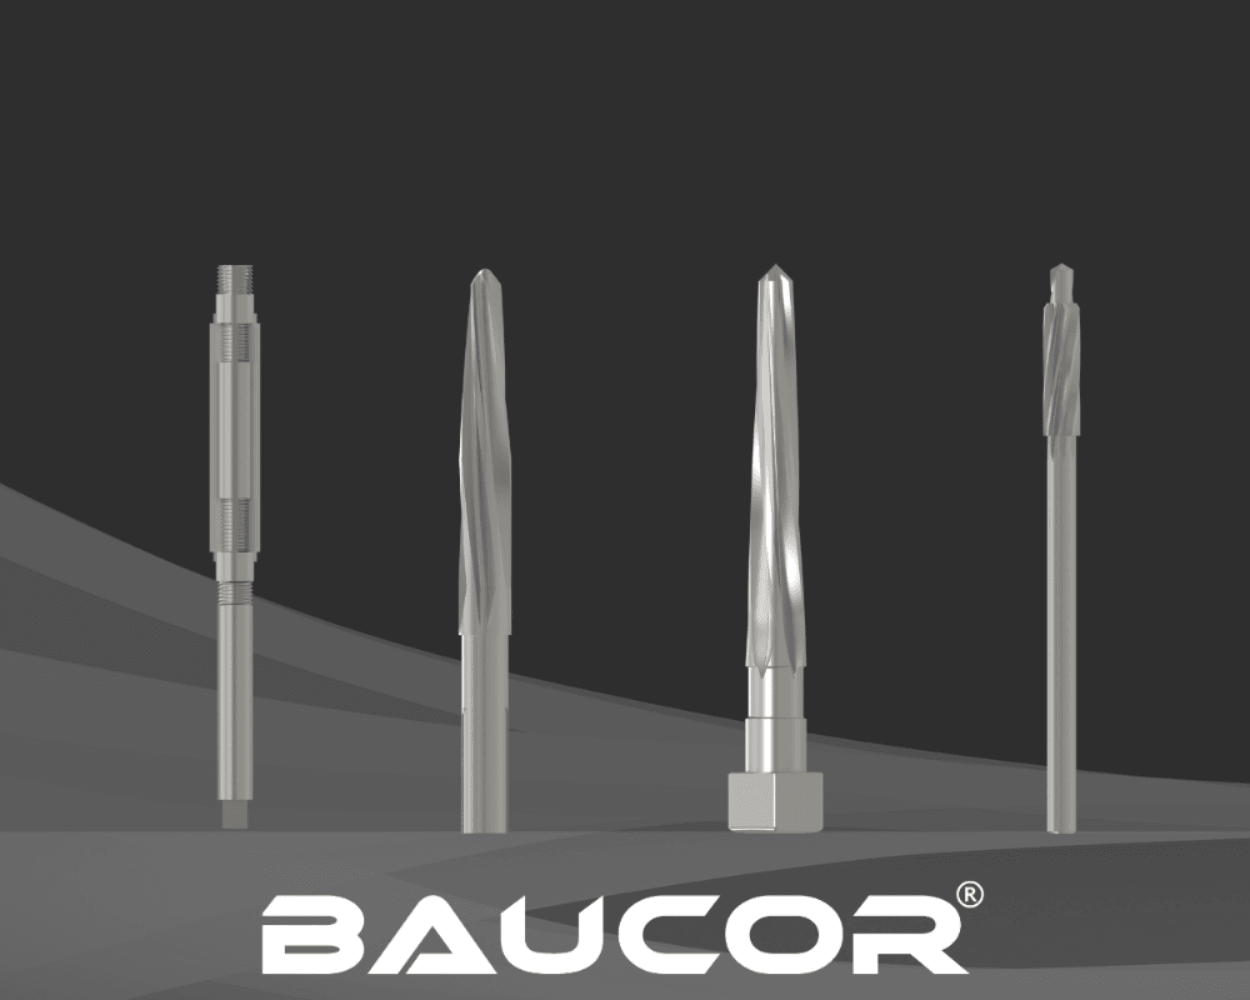
Baucor manufactures hand reamers in HSS, cobalt HSS and carbide, with straight or spiral flutes, in metric and inch sizes. We also make custom hand reamers to your diameter, tolerance and length.
What is a hand reamer used for?
Use a hand reamer when a hole must be precise but a machine isn't practical: in assembly, maintenance and repair, on large parts that can't go on a machine, or for a small number of holes.
Typical job
Example
Fitting dowel and taper pins
Aligning machine parts, fixtures and dies
Sizing holes for bushings and bearings
Press fits and slip fits in repair work
Correcting holes in assemblies
Line-reaming holes in parts already bolted together
Finishing holes in large or fixed parts
Frames, castings and housings that can't be moved to a machine
Toolroom and maintenance work
One-off holes, prototypes, worn holes
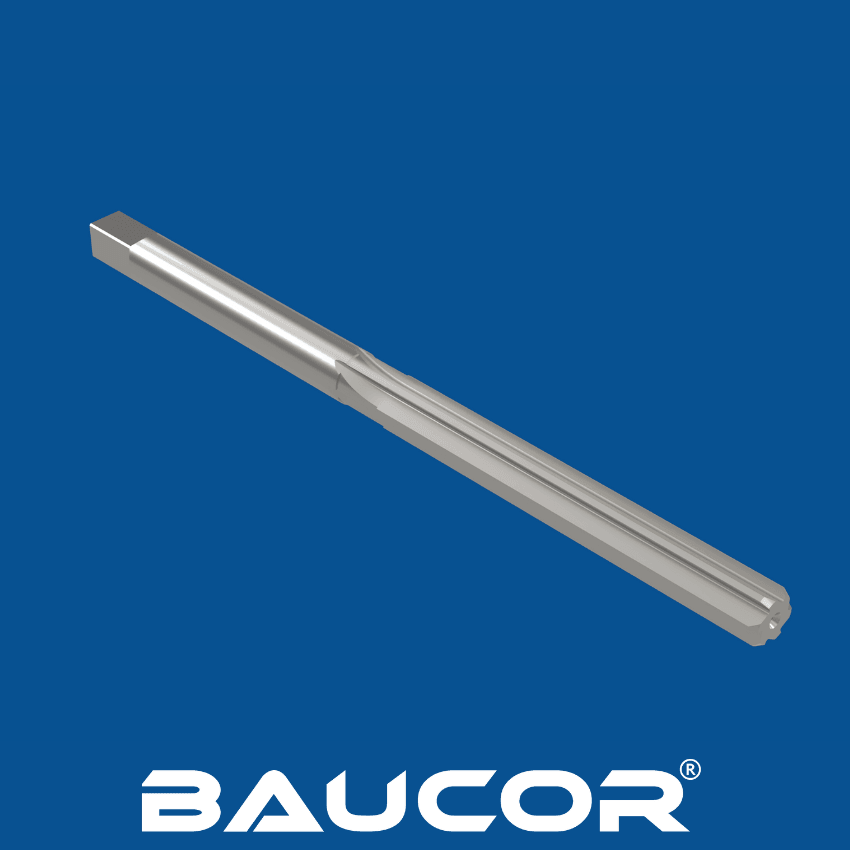
Anatomy of a hand reamer
Part
What it does
Square drive
Fits a tap wrench, so the reamer can be turned by hand with even pressure
Shank
Plain section between the drive and the flutes; the diameter is usually slightly under the cutting size
Taper lead (starting taper)
A long, gentle taper at the front, typically over about a quarter of the flute length. It centers the reamer in the hole and spreads the cut over many teeth
Flutes
Straight or spiral grooves that form the cutting edges and carry chips away
Cutting edges / margins
Remove a thin layer of material and burnish the hole wall; many hand reamers use uneven tooth spacing to reduce chatter
The long taper lead is what makes a hand reamer self-centering.
Hand reamer vs machine reamer
Hand reamer
Machine (chucking) reamer
Driven by
Tap wrench, by hand
Drill press, lathe, mill or CNC
Shank end
Square drive
Straight or Morse taper shank
Front of the tool
Long taper lead
Short 45° chamfer
Material removed
Very little
More
Speed
Slow, controlled
Machine speed and feed
Best for
Assembly, repair, few holes, large parts
Production, many identical holes
Never use a hand reamer in a power drill. The long taper and square drive are not designed for machine speeds; the reamer will chatter, cut oversize and can break. For machine reaming, use machine reamers or chucking reamers.
Straight or spiral flute hand reamer?
Straight flute
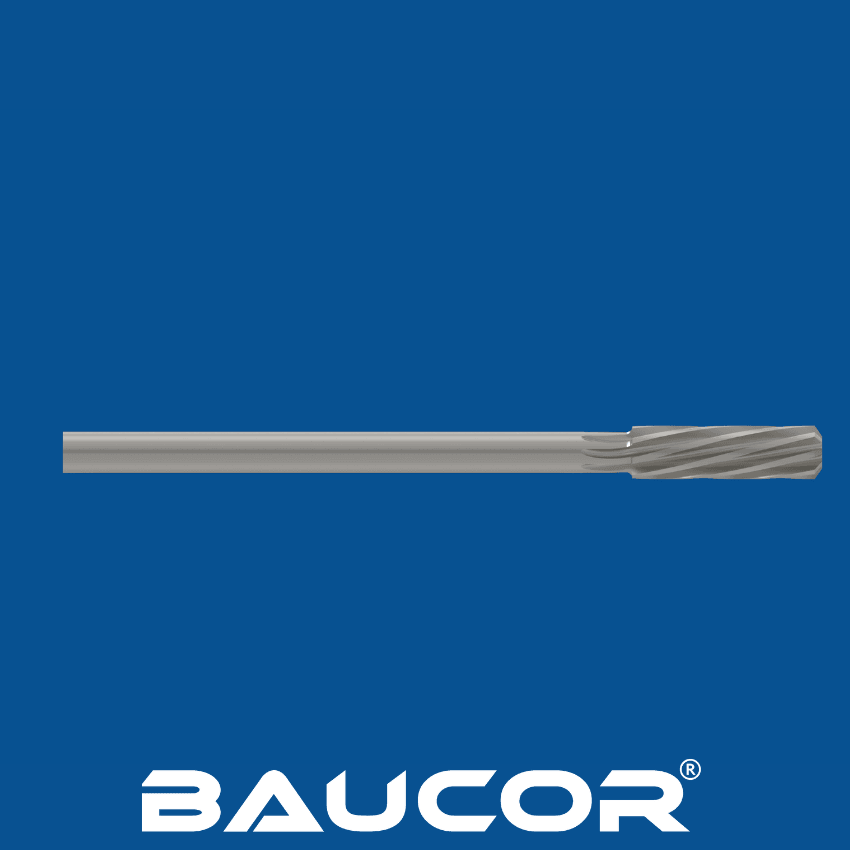
Left-hand spiral flute
Best for
General work, blind holes, cast iron, brass
Holes with keyways, slots or cross-holes (interrupted cuts); through holes
Chip flow
Chips stay in the flutes
Pushes chips forward, ahead of the reamer
Cutting behavior
Simple, easy to control
Smoother cut; the left-hand spiral stops the reamer from screwing itself into the hole
Drill the hole undersize. Use the stock allowance table below.
Deburr the hole entry so the taper lead starts cleanly.
Fit the reamer in a tap wrench and place it square to the hole. Check with a square for the first turns.
Apply cutting fluid (steel and stainless). Cast iron and brass are usually reamed dry.
Turn clockwise only, slowly and evenly, with light downward pressure. Let the taper lead guide the tool.
Never turn backwards, not even to remove the reamer. Turning in reverse dulls the cutting edges and scratches the hole.
Remove the reamer by continuing to turn clockwise while pulling it out, or push it through a through-hole.
Clean and check the hole with a plug gauge or the mating part.
Stock allowance: how much undersize to drill
Reamer diameter
Material to leave for hand reaming (on diameter)
Example drill size
Up to 6 mm
0.1 mm (0.004 in)
6 mm reamer → 5.9 mm drill
6 – 12 mm
0.1 – 0.2 mm (0.004 – 0.008 in)
10 mm reamer → 9.8 mm drill
12 – 25 mm
0.2 – 0.3 mm (0.008 – 0.012 in)
20 mm reamer → 19.75 mm drill
Over 25 mm
0.3 mm (0.012 in)
30 mm reamer → 29.7 mm drill
These are typical values for hand reaming. Leave less in hard materials and more in soft, gummy ones. Too little material makes the reamer rub instead of cut; too much overloads it and the hole ends up oversize or rough.
Troubleshooting: common hand reaming problems
Problem
Likely cause
Fix
Hole is oversize
Reamer not square to the hole; too much stock; worn or damaged reamer
A hand reamer is a manual cutting tool, turned with a tap wrench, that finishes a pre-drilled hole to an exact diameter and a smooth surface. It has a square drive and a long taper lead that centers it in the hole.
What size drill should I use before a hand reamer?
Drill slightly undersize: about 0.1 mm smaller for reamers up to 6 mm, 0.1–0.2 mm for 6–12 mm, and 0.2–0.3 mm for 12–25 mm. For example, drill 9.8 mm for a 10 mm hand reamer.
Can I use a hand reamer in a drill?
No. Hand reamers are designed for slow, manual turning. In a power drill they chatter, cut oversize and can break. Use a machine or chucking reamer instead.
What is the difference between a hand reamer and a machine reamer?
A hand reamer has a square drive and a long taper lead for manual use. A machine reamer has a straight or Morse taper shank and a short chamfer, and runs in a drill press, lathe or CNC machine.
Should I choose a straight or spiral flute hand reamer?
Choose straight flutes for general work and blind holes. Choose a left-hand spiral flute for holes with keyways or cross-holes, because it cuts smoothly over the gaps and won't screw itself into the hole.
Why should you never turn a reamer backwards?
Turning backwards drags chips across the cutting edges. This dulls the reamer and scratches the hole wall. Always keep turning clockwise, also while removing it.
What tolerance does a hand reamer produce?
Standard hand reamers are made to produce H7 holes, a common fit for dowel pins and bearings. Baucor can make hand reamers for other tolerance classes on request.
Why Baucor hand reamers
Manufactured to H7 tolerance with ground cutting edges.
Standard sizes and custom hand reamers from one supplier.
Engineering support from Baucor's tooling team in Irvine, CA and Mannheim, Germany.
Whether you need a single prototype or full-scale production, Baucor''s engineers are ready to collaborate with you. Contact us to discuss how we can bring your concept to life.
Tailored Solutions for Baucor Customers
Baucor specializes in providing unique manufacturing and engineering solutions designed to meet the specific needs of each client. Our expertise covers a wide range of industries and applications.